Cream Pump Manufacturer - Quality Dispensing

All Categories

cream pump manufacturer

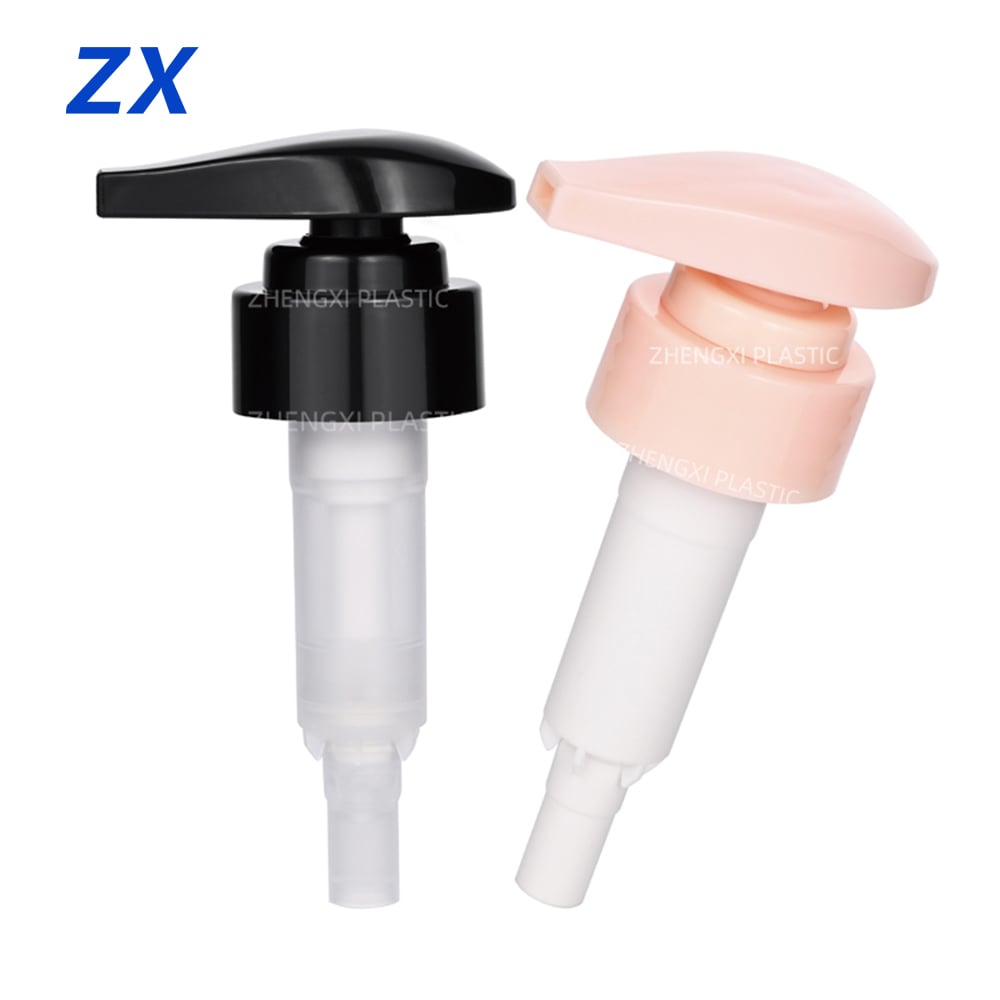
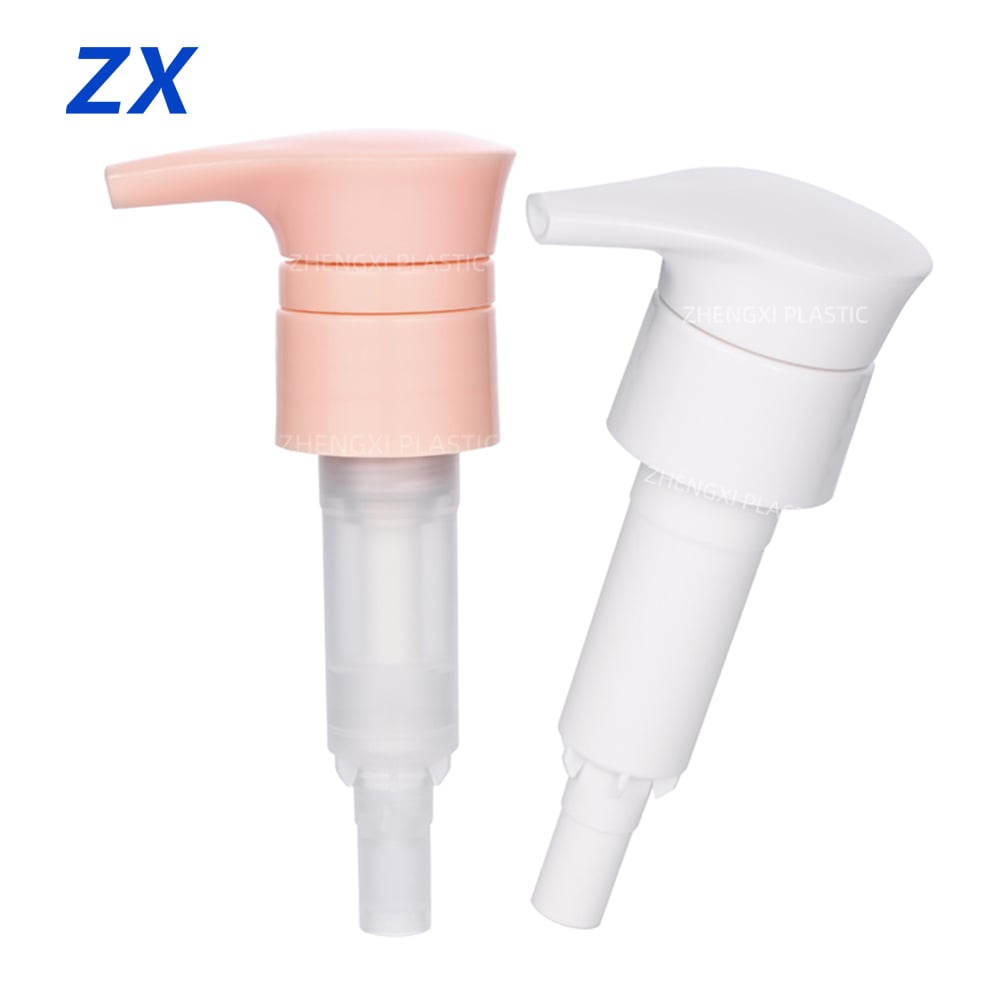
A cream pump manufacturer specializes in designing and producing precision dispensing systems for cosmetic and personal care products. These manufacturers create pump mechanisms that deliver controlled amounts of creams, lotions, and similar viscous formulations with each press. The main function centers on providing hygienic, convenient, and waste-reducing dispensing solutions for beauty and skincare products. A quality cream pump manufacturer employs advanced engineering to ensure consistent dosage delivery, preventing product contamination and extending shelf life. Technological features include airless pump technology that protects sensitive formulations from oxidation, lockable mechanisms for travel safety, and customizable actuators that accommodate various container sizes. These manufacturers utilize materials such as polypropylene, stainless steel, and FDA-approved plastics to ensure product safety and compatibility. Applications span across facial moisturizers, body lotions, anti-aging serums, foundation creams, and pharmaceutical topicals. The cream pump manufacturer serves brands ranging from luxury cosmetics to mass-market personal care companies, offering solutions that enhance user experience and brand presentation. Manufacturing capabilities typically include injection molding, assembly automation, and quality testing protocols that verify pump performance across thousands of cycles. A reliable cream pump manufacturer provides customization options including color matching, printing capabilities, and various pump output volumes to meet specific brand requirements and product viscosities.

New Product Recommendations

Partnering with an experienced cream pump manufacturer delivers multiple practical benefits that directly impact your product success and customer satisfaction. First, you gain access to superior dispensing technology that ensures accurate product dosage with every use, reducing waste and providing better value to your customers. This precision helps control product consumption and extends the lifespan of each container, which customers appreciate and remember when making repeat purchases. Working with a specialized cream pump manufacturer means receiving expert guidance on pump selection based on your specific formulation viscosity, container design, and target market preferences. You benefit from economies of scale in production, receiving competitive pricing without compromising quality standards. The manufacturer handles complex engineering challenges, allowing you to focus on product development and marketing rather than dispensing mechanics. Quality assurance protocols employed by professional cream pump manufacturers ensure reliability across millions of actuations, minimizing customer complaints and return rates. You also receive contamination prevention through sealed pump systems that keep bacteria and air away from your formulations, particularly crucial for preservative-free or natural products. A credible cream pump manufacturer offers design flexibility, enabling you to differentiate your packaging and create memorable unboxing experiences. Speed to market improves significantly when working with established manufacturers who maintain ready inventory of standard components and can quickly prototype custom solutions. Additionally, compliance support ensures your dispensing systems meet regional safety regulations and industry standards, protecting your brand reputation and avoiding costly recalls.

Latest News

Together We Grow, Together We Shine | Zhengxi Packaging Successfully Held Its 2025 Annual Meeting

17

Jun

Together We Grow, Together We Shine | Zhengxi Packaging Successfully Held Its 2025 Annual Meeting

View More
Zhengxi Successfully Exhibited at Cosmoprof Bologna 2026 – Showcasing Innovative Pump Packaging Solutions and Expanding Global Partnerships

17

Jun

Zhengxi Successfully Exhibited at Cosmoprof Bologna 2026 – Showcasing Innovative Pump Packaging Solutions and Expanding Global Partnerships

View More
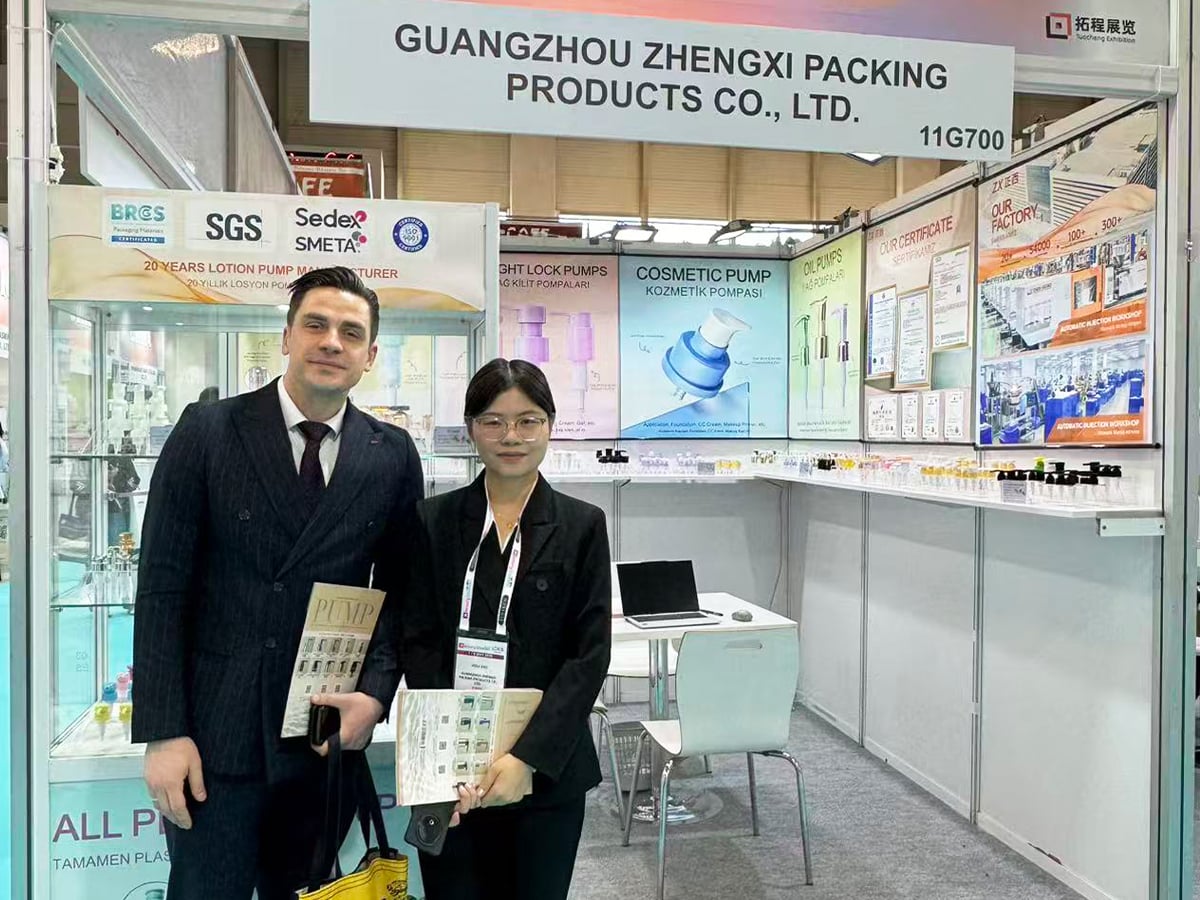
Successful Participation: Zhengxi Packaging Shines at Beauty Istanbul 2026

17

Jun

Successful Participation: Zhengxi Packaging Shines at Beauty Istanbul 2026

View More
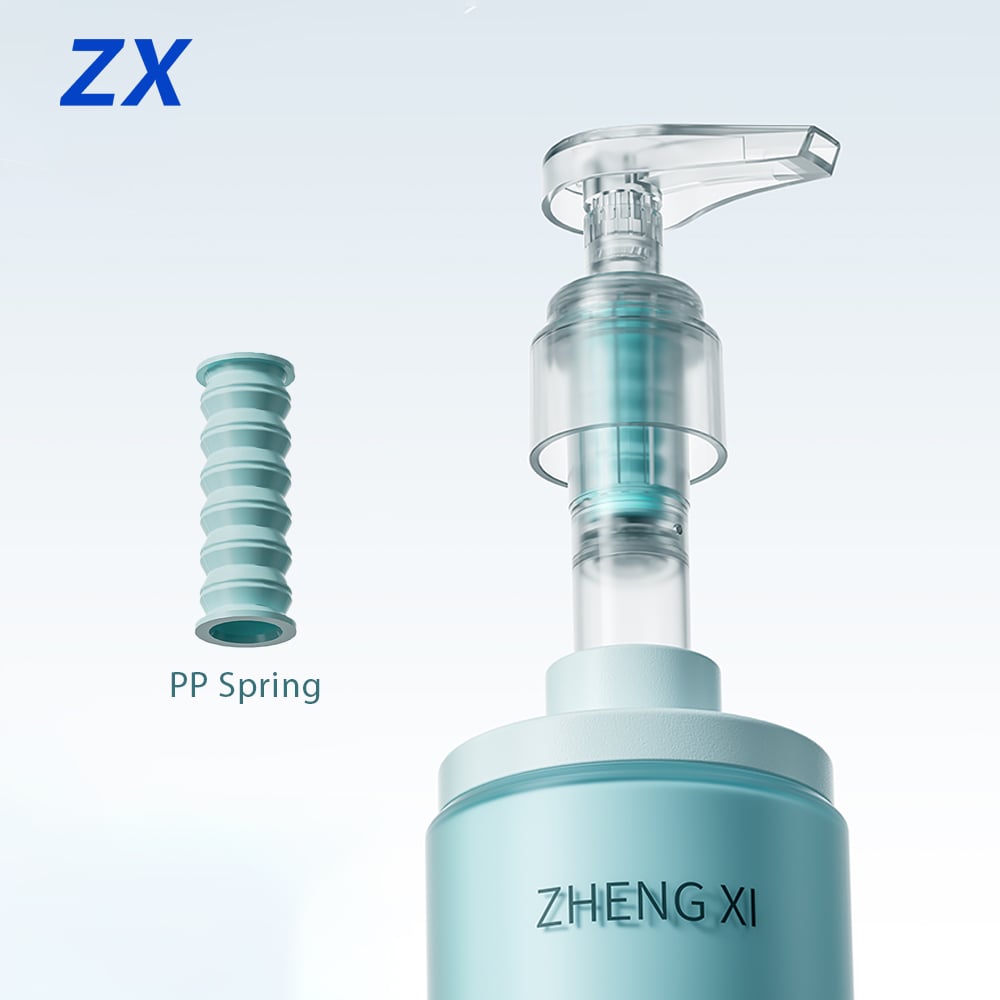
What are the internal components of a lotion pump dispenser and how does it function?

30

Jun

What are the internal components of a lotion pump dispenser and how does it function?

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

cream pump manufacturer

Advanced Airless Pump Technology

Advanced Airless Pump Technology

Modern cream pump manufacturers have developed sophisticated airless dispensing systems that revolutionize product preservation and user experience. This technology creates a vacuum environment inside the container, completely eliminating air exposure that causes oxidation and degradation of active ingredients. When you select a cream pump manufacturer offering airless solutions, your formulations maintain potency and efficacy throughout the product lifecycle. The airless mechanism works through a piston at the container base that rises as product dispenses, ensuring virtually complete evacuation with minimal waste remaining in the bottle. This feature particularly benefits premium skincare brands where expensive active ingredients justify the investment in superior dispensing technology. Customers notice the difference immediately through consistent texture and performance from first use to last drop. The cream pump manufacturer designs these systems with precision-engineered components that create perfect seals, preventing backflow and maintaining the vacuum integrity. This technology also enables preservative-reduction in formulations since microbial contamination risks decrease substantially without air exposure. Brands utilizing airless pumps from a quality cream pump manufacturer can market longer shelf life and cleaner ingredient lists, both increasingly important to conscious consumers.
Customization and Brand Differentiation

Customization and Brand Differentiation

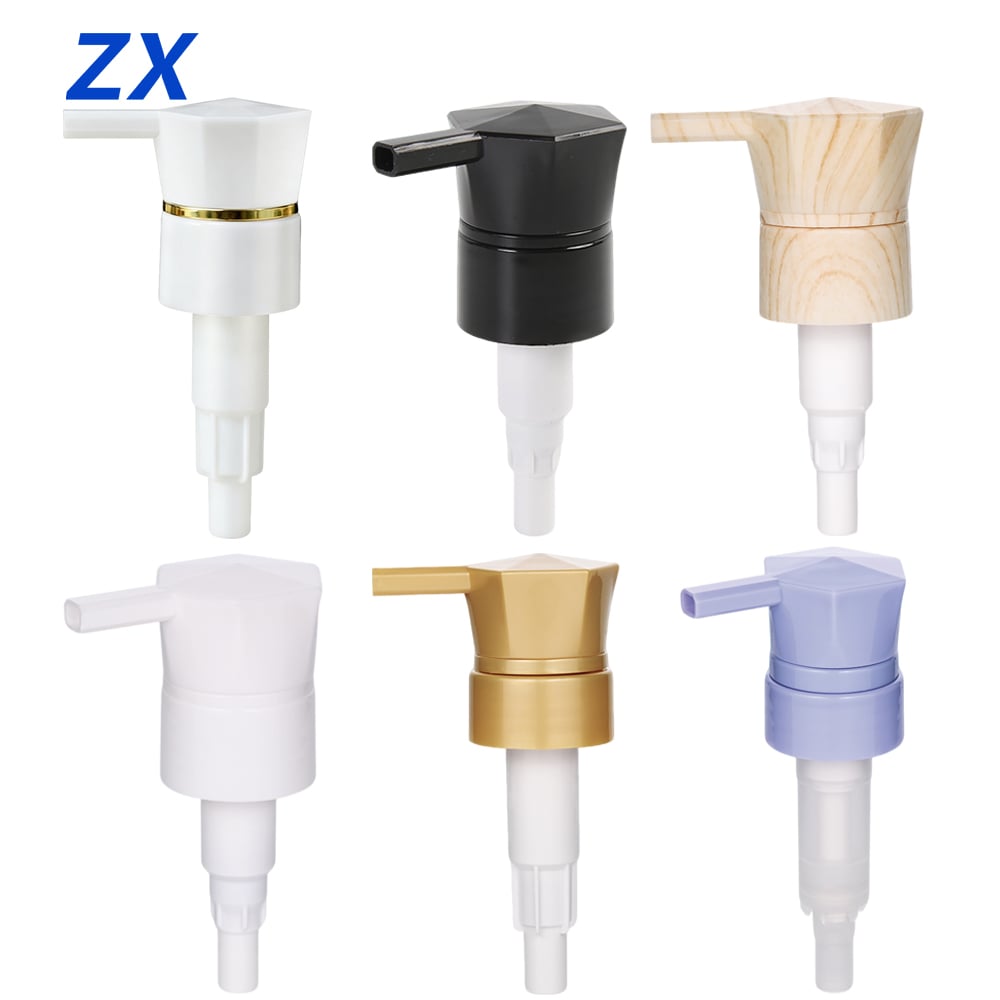
A versatile cream pump manufacturer offers extensive customization capabilities that transform standard dispensing components into distinctive brand assets. Customization begins with actuator design, where manufacturers can create unique shapes, textures, and ergonomic profiles that become recognizable brand signatures. Color matching services allow precise coordination with your overall packaging aesthetic, whether achieving specific Pantone shades or metallic finishes that convey luxury positioning. Surface treatments including matte, glossy, soft-touch, or metallic coatings add tactile dimensions that enhance perceived value. The cream pump manufacturer can incorporate your logo directly onto pump components through pad printing, hot stamping, or laser etching, creating cohesive branding across every product element. Output volume customization ensures the pump delivers the optimal amount for your specific product application, whether a light facial serum requiring small doses or rich body cream needing larger dispensing. Collar and overcap designs receive equal attention, with options for different closure mechanisms and decorative elements. Working closely with your cream pump manufacturer during development phases allows creation of proprietary pump designs that competitors cannot replicate, establishing strong visual differentiation on crowded retail shelves and building long-term brand equity through consistent, quality dispensing experiences.
Rigorous Quality Control and Compliance

Rigorous Quality Control and Compliance

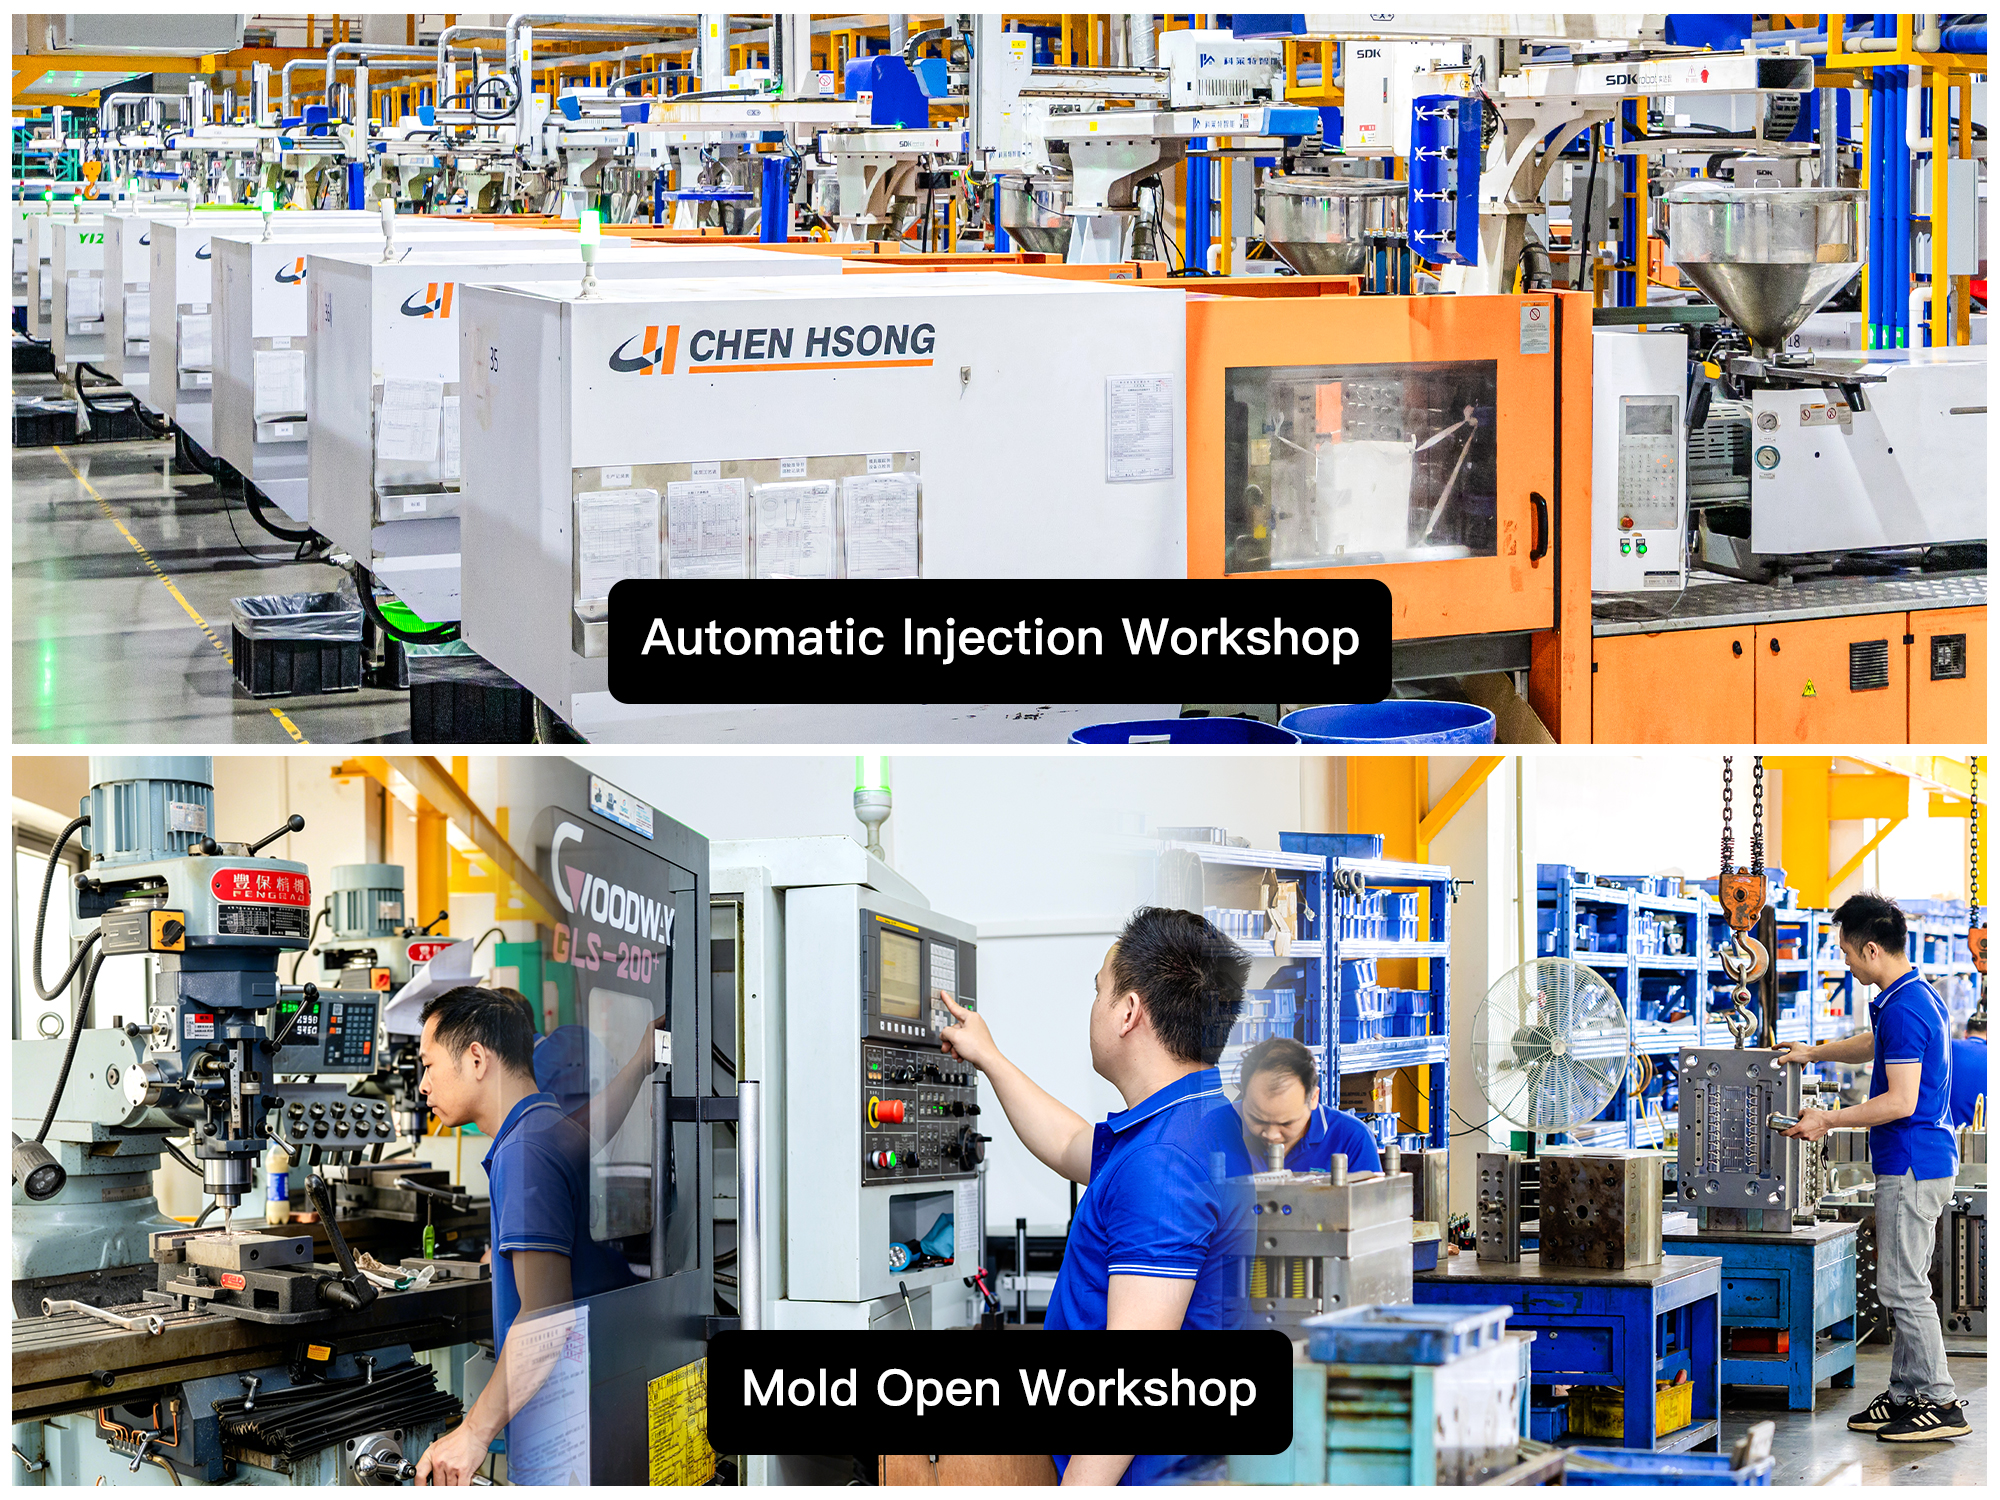
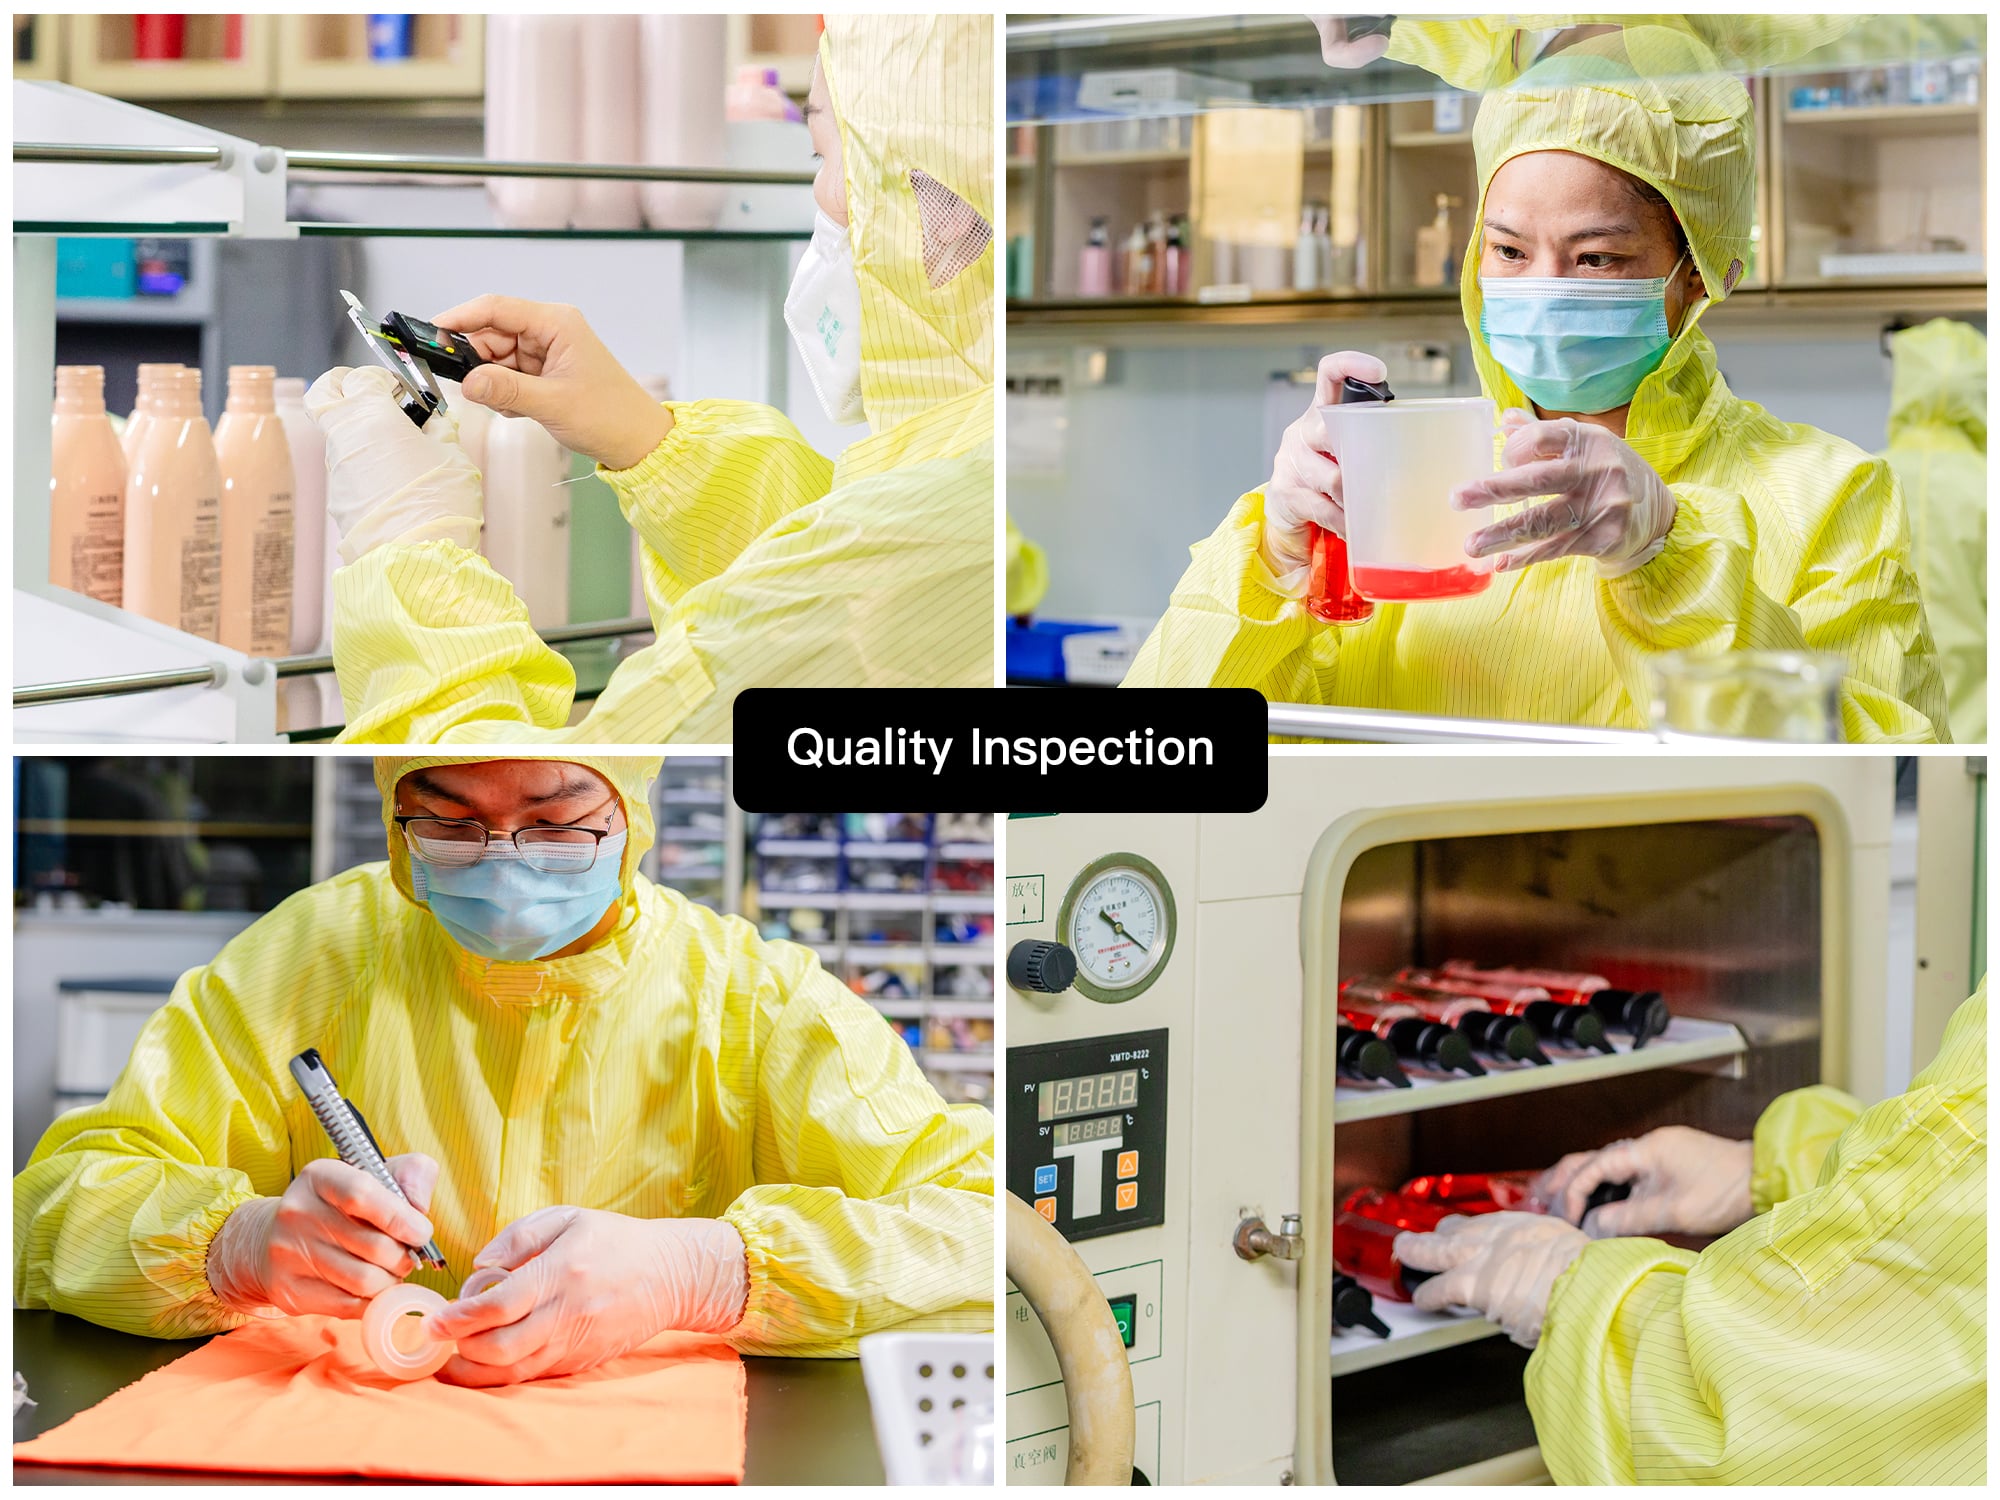
Professional cream pump manufacturers implement comprehensive quality control systems that protect brand reputation and ensure consistent performance across production volumes. Testing protocols begin with raw material verification, confirming that all plastics, springs, and sealing components meet specified standards before entering production. During manufacturing, the cream pump manufacturer conducts in-process inspections at critical assembly stages, catching potential defects before they become finished goods. Functional testing subjects pumps to thousands of actuation cycles under varying temperatures and pressures, simulating years of consumer use to identify potential failure points. Compatibility testing ensures pump materials do not react adversely with different formulation types, preventing discoloration, degradation, or chemical leaching that could compromise product safety. Drop testing and stress analysis verify that assembled pumps withstand distribution challenges and typical handling scenarios. A responsible cream pump manufacturer maintains detailed documentation for traceability, allowing rapid identification and isolation of any quality issues. Regulatory compliance expertise proves invaluable as manufacturers stay current with FDA regulations, EU cosmetics directives, and international safety standards. Certifications such as ISO 9001 quality management and ISO 14001 environmental standards demonstrate commitment to operational excellence. This comprehensive quality framework minimizes risk, reduces waste, and ensures every pump leaving the cream pump manufacturer meets exacting specifications.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000