Shampoo Pump Factory - Quality Manufacturing

All Categories

shampoo pump factory

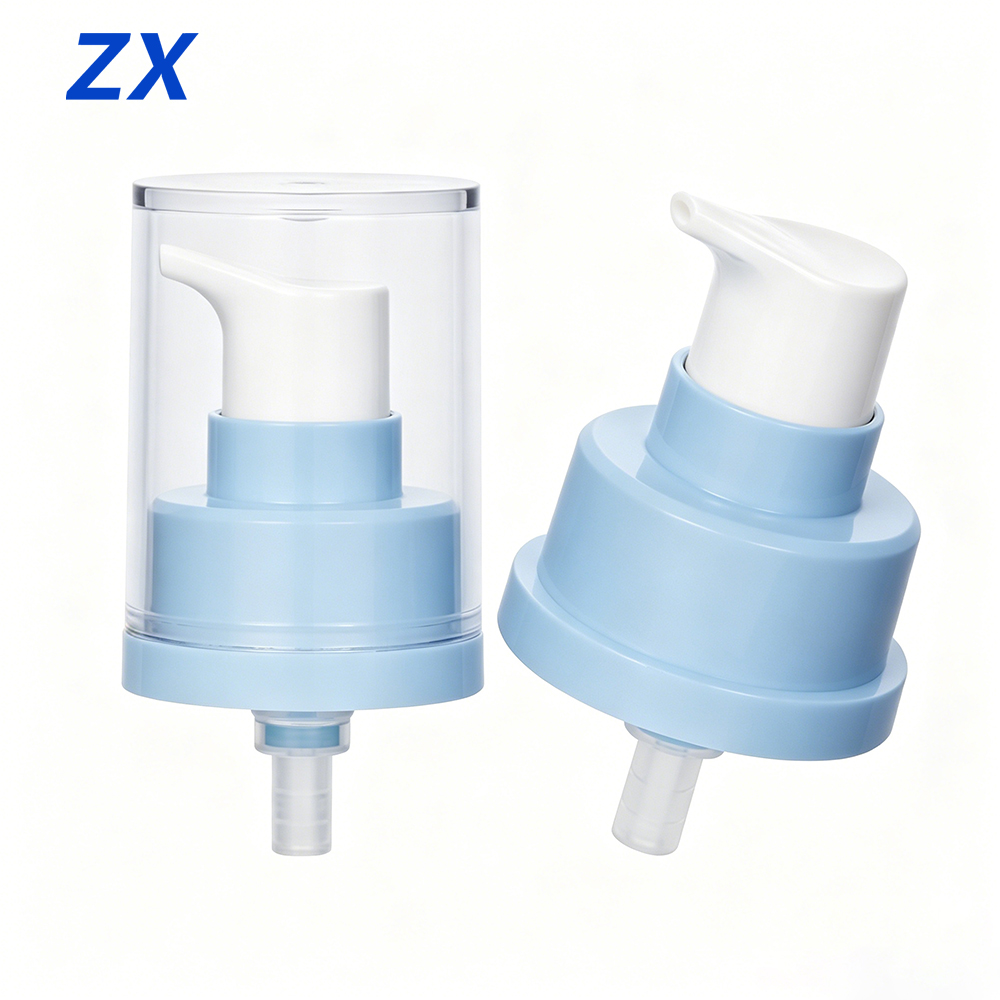
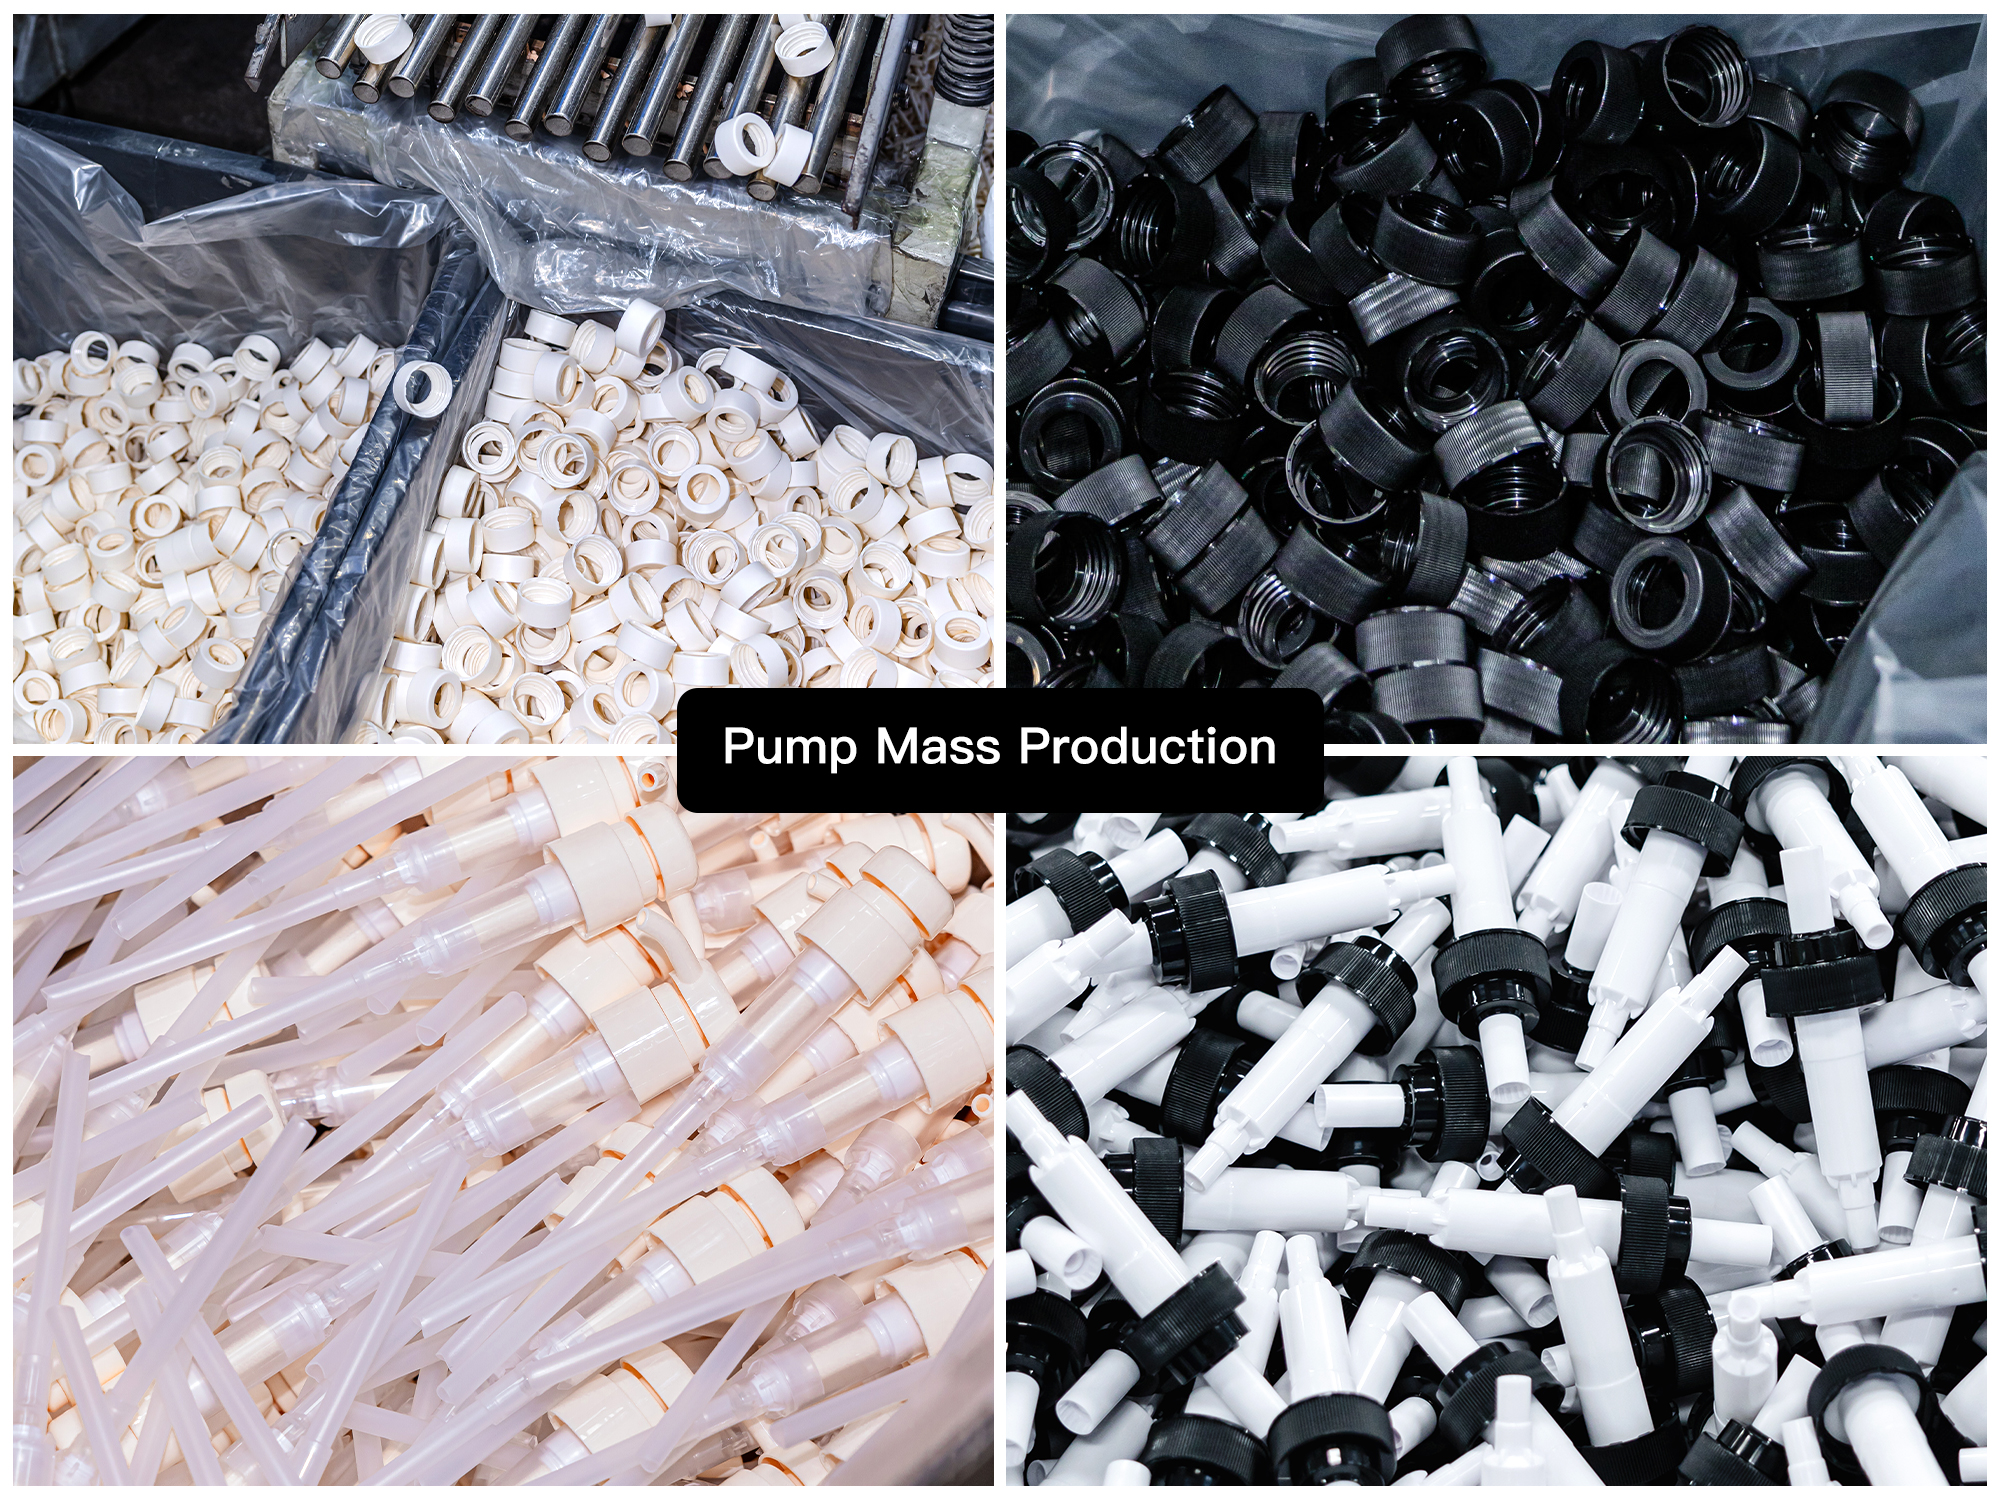
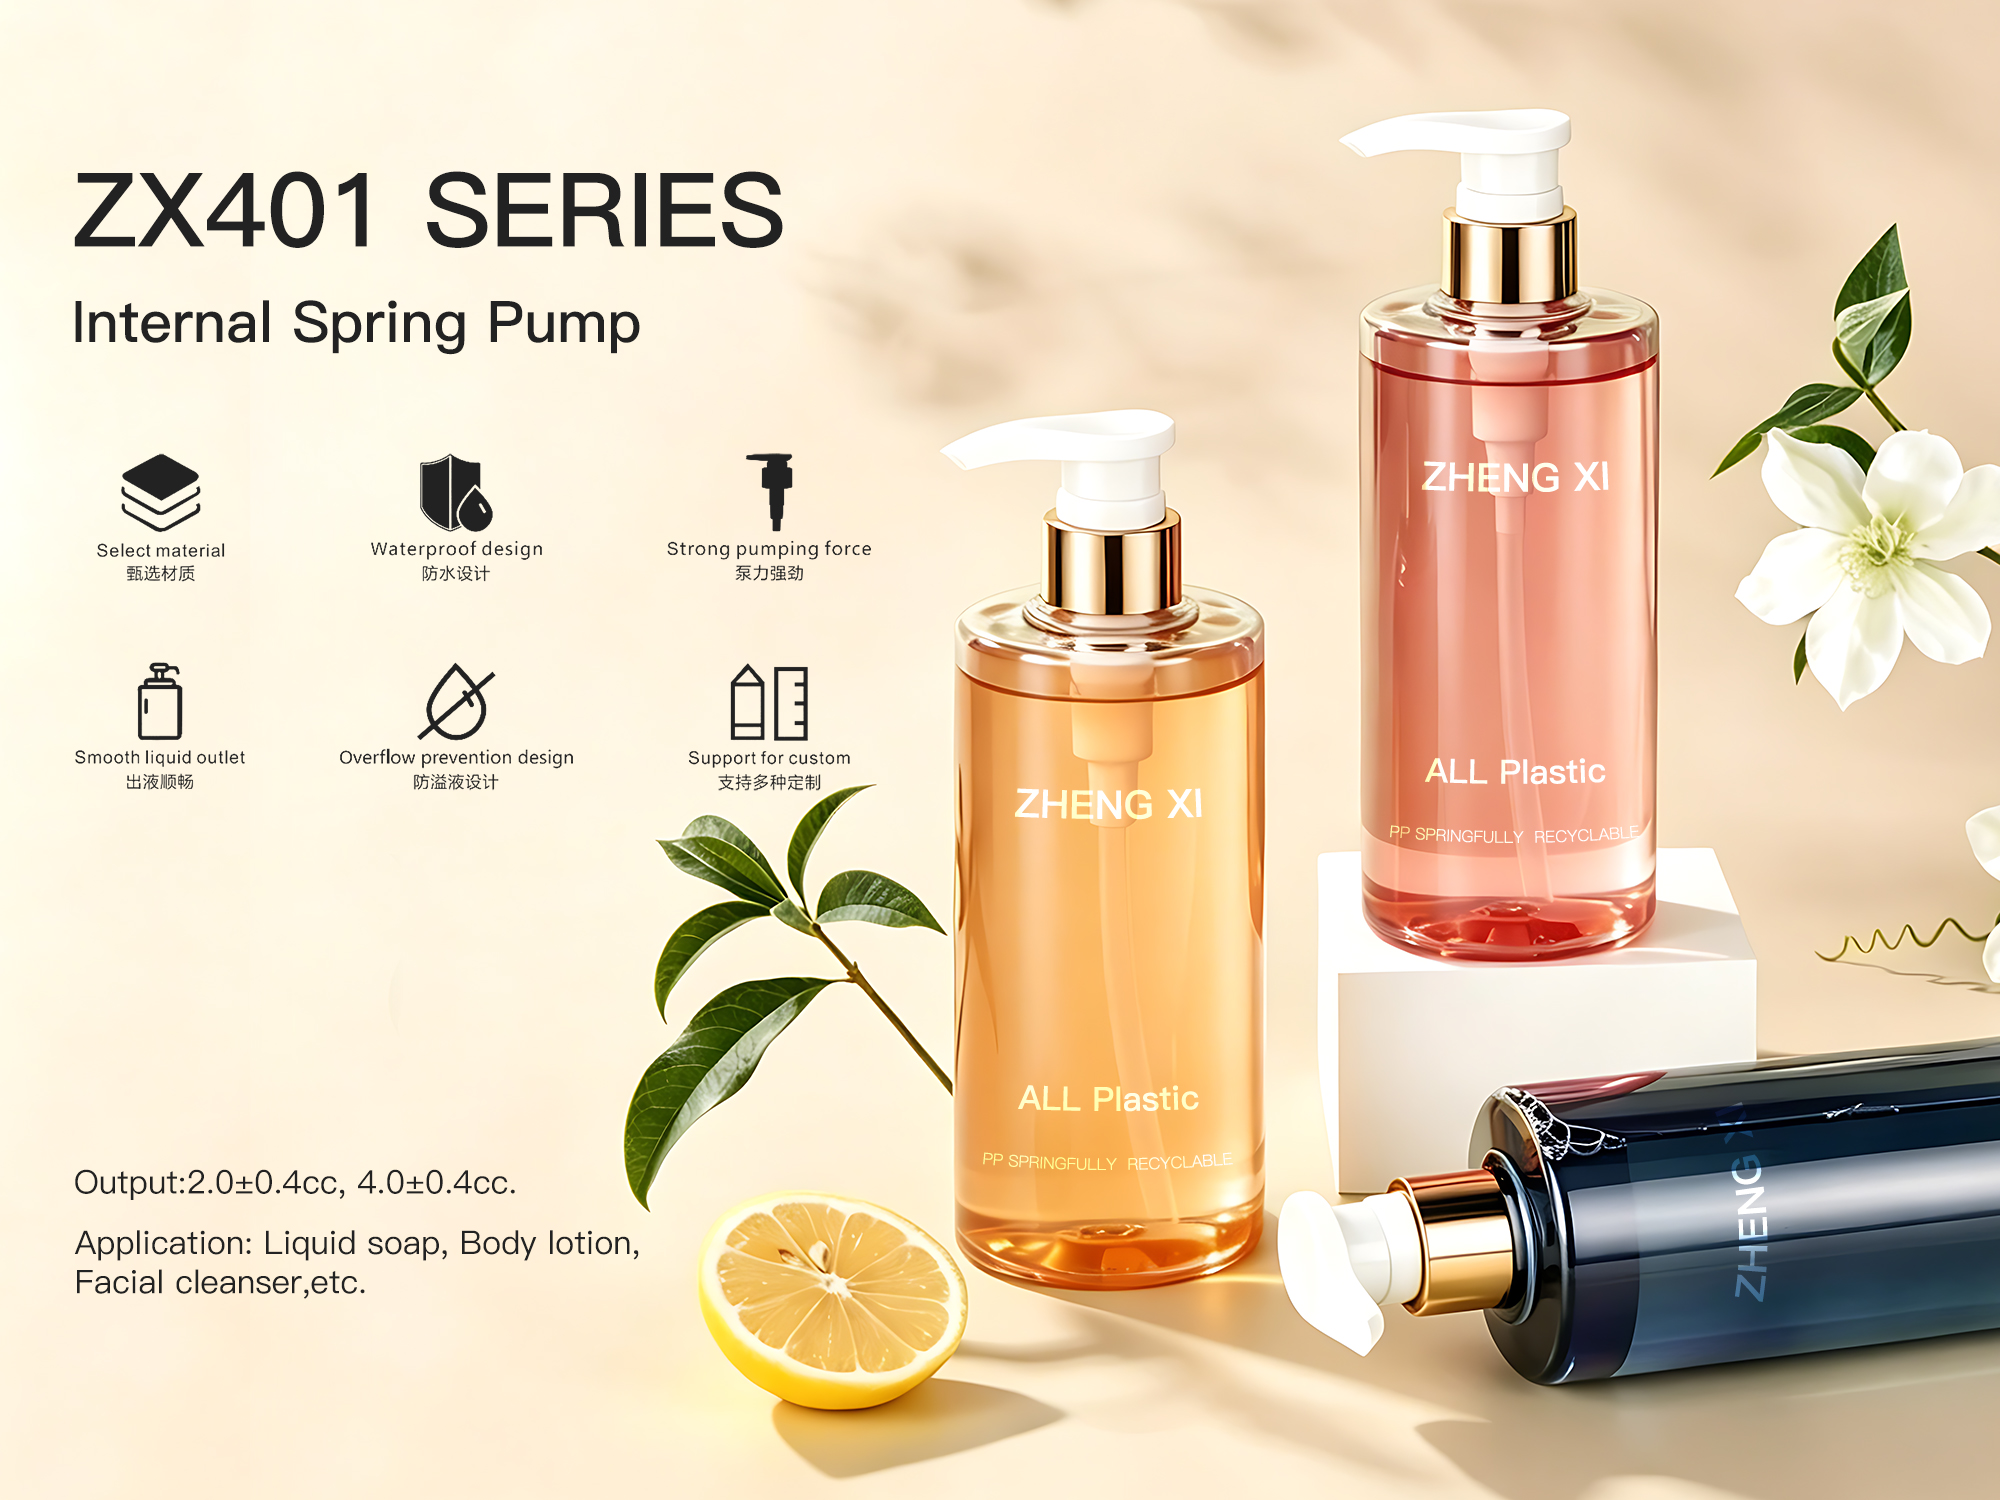
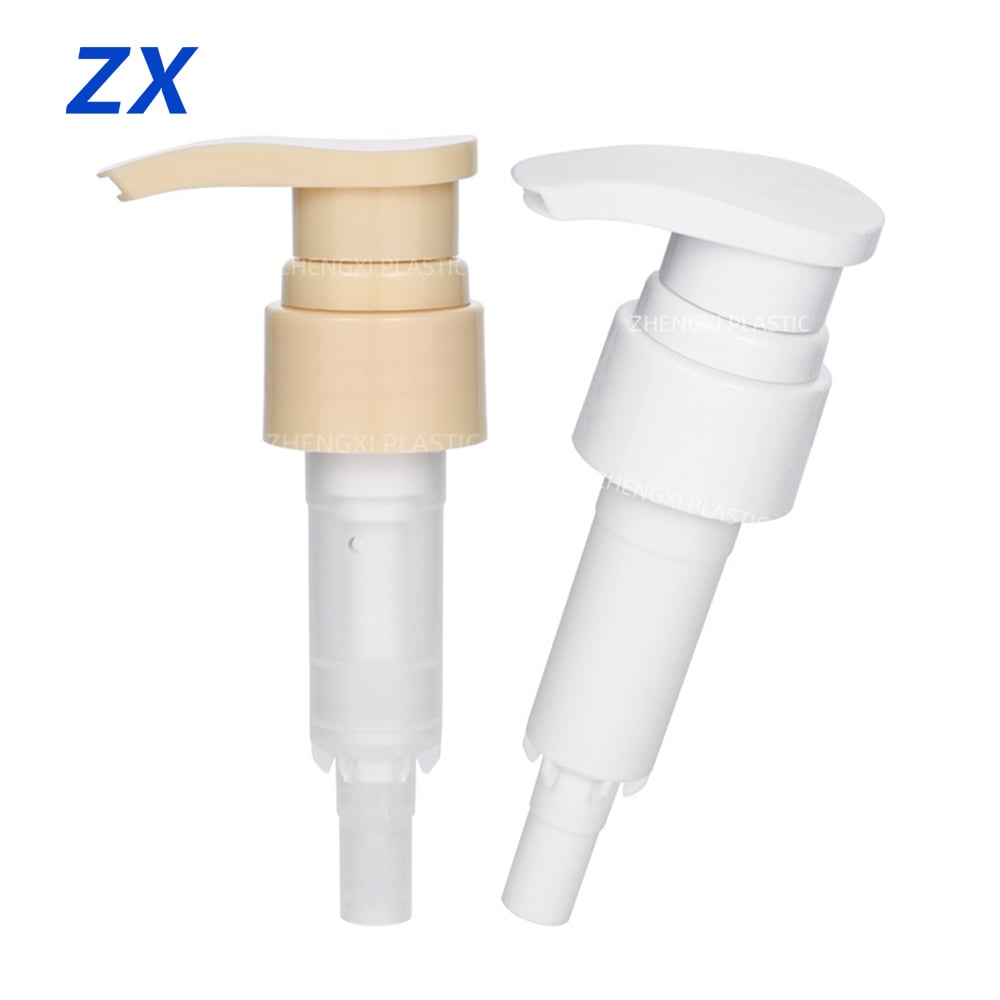
A shampoo pump factory specializes in manufacturing precision dispensing mechanisms designed specifically for personal care and cosmetic products. These facilities produce high-quality pump dispensers that control the flow of liquid shampoo, conditioner, and similar viscous products with consistent accuracy. Modern shampoo pump factory operations integrate advanced molding technologies, automated assembly lines, and rigorous quality control systems to ensure each pump meets international standards for hygiene and performance. The primary function of a shampoo pump factory is to deliver reliable dispensing solutions that enhance user experience while maintaining product integrity. These pumps typically feature spring-loaded mechanisms, dip tubes, and precisely engineered nozzles that create optimal dosage control. Manufacturing processes within a shampoo pump factory include injection molding of plastic components, spring insertion, valve assembly, and final testing procedures. The technological features encompass corrosion-resistant materials, leak-proof sealing systems, and customizable output volumes ranging from 1ml to 4ml per stroke. Applications extend across residential bathrooms, professional salons, hospitality industries, and retail packaging for premium hair care brands. A professional shampoo pump factory serves cosmetic manufacturers, private label producers, and packaging companies seeking dependable dispensing hardware. The factory environment maintains strict cleanliness protocols to prevent contamination and ensure each pump component meets pharmaceutical-grade standards suitable for direct contact with personal care formulations.

Popular Products

Partnering with a dedicated shampoo pump factory provides significant cost advantages through economies of scale and streamlined production workflows. Bulk manufacturing capabilities reduce per-unit costs substantially, allowing buyers to maximize profit margins while maintaining competitive retail pricing. Operational benefits include consistent supply chain reliability, with established factories maintaining adequate inventory levels and predictable lead times that prevent stock shortages during peak demand periods. Quality assurance processes within a professional shampoo pump factory eliminate the risks associated with defective dispensers, reducing product returns and protecting brand reputation. Factories equipped with modern testing equipment verify each pump's functionality, ensuring proper dosage delivery and smooth actuation across thousands of cycles. Application suitability extends to various viscosity levels, with specialized shampoo pump factory designs accommodating thin serums, standard shampoos, and thick conditioning treatments without performance degradation. Customization options available from experienced factories enable brand differentiation through color matching, logo printing, and unique actuator designs that enhance shelf appeal. Working directly with a shampoo pump factory provides access to technical expertise, helping buyers select appropriate pump specifications for their specific formulations and container designs. Environmental considerations are increasingly important, with many factories now offering recyclable materials and refillable pump systems that align with sustainability goals. The decision to source from an established shampoo pump factory rather than intermediaries provides better pricing transparency, improved communication channels, and faster resolution of technical issues. Factories with certification standards ensure compliance with regional regulations governing cosmetic packaging, simplifying market entry across different geographical regions and reducing legal risks for buyers.

Practical Tips

Together We Grow, Together We Shine | Zhengxi Packaging Successfully Held Its 2025 Annual Meeting

17

Jun

Together We Grow, Together We Shine | Zhengxi Packaging Successfully Held Its 2025 Annual Meeting

View More
What are the internal components of a lotion pump dispenser and how does it function?

30

Jun

What are the internal components of a lotion pump dispenser and how does it function?

View More
How to customize a treatment pump with a child-resistant lock for safety compliance?

30

Jun

How to customize a treatment pump with a child-resistant lock for safety compliance?

View More
What To Consider When Purchasing Lotion Dispensing Pumps for Bottles?

30

Jun

What To Consider When Purchasing Lotion Dispensing Pumps for Bottles?

View More

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

shampoo pump factory

Advanced Manufacturing Precision and Quality Control

Advanced Manufacturing Precision and Quality Control

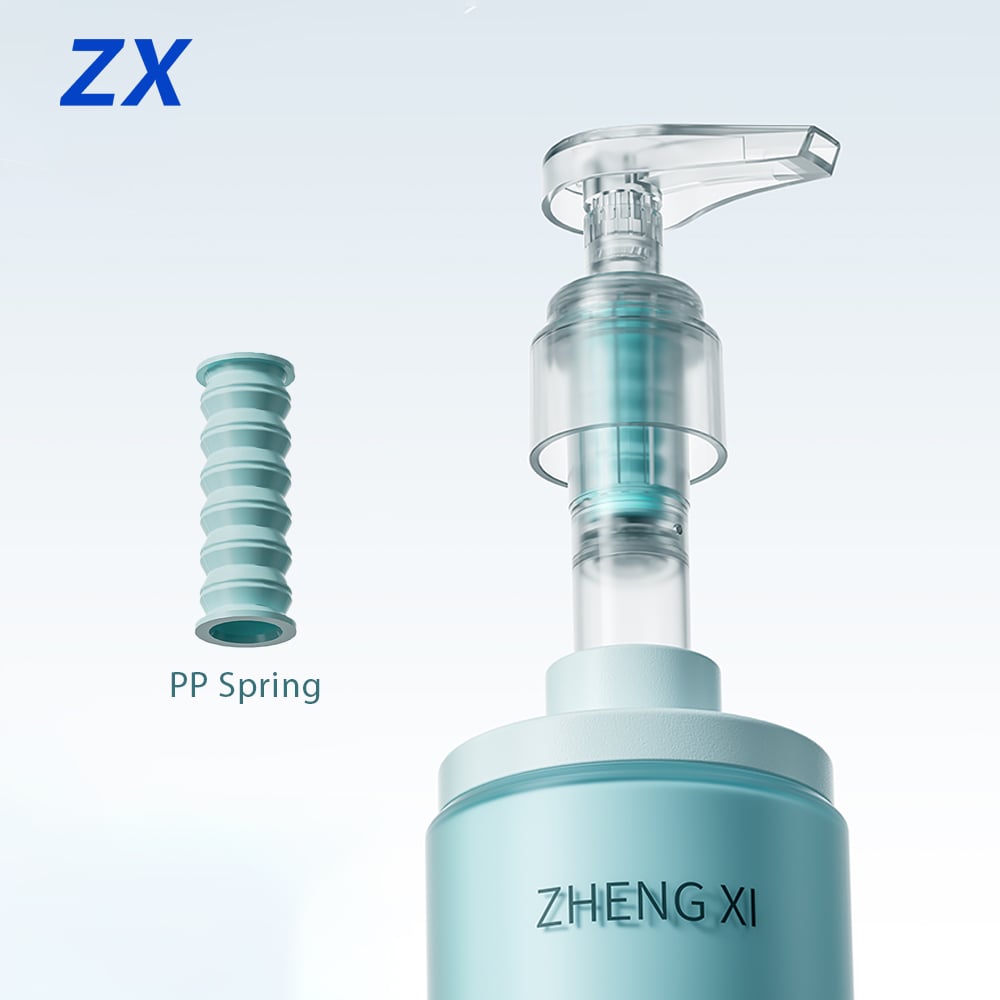
A professional shampoo pump factory employs sophisticated manufacturing technologies that guarantee consistent product quality across large production volumes. Computer-controlled injection molding machines create pump components with micron-level precision, ensuring perfect fit tolerances that prevent leakage and maintain smooth operation throughout the product lifecycle. Automated assembly lines equipped with vision inspection systems detect even minor defects, removing substandard units before packaging. This technological infrastructure within a shampoo pump factory significantly reduces variability compared to manual assembly processes. Spring tension calibration equipment ensures uniform dispensing pressure, delivering the same product volume with each actuation regardless of container fullness. Material selection processes prioritize food-grade polypropylene and polyethylene resins that resist chemical degradation from sulfates, silicones, and preservatives commonly found in shampoo formulations. The quality assurance protocols include cycle testing that simulates years of normal usage, pressure testing to verify seal integrity, and drop testing to confirm structural durability during shipping and handling. These comprehensive quality measures protect buyers from costly recalls and customer complaints while establishing the shampoo pump factory as a trusted partner in product development.
Customization Flexibility for Brand Differentiation

Customization Flexibility for Brand Differentiation

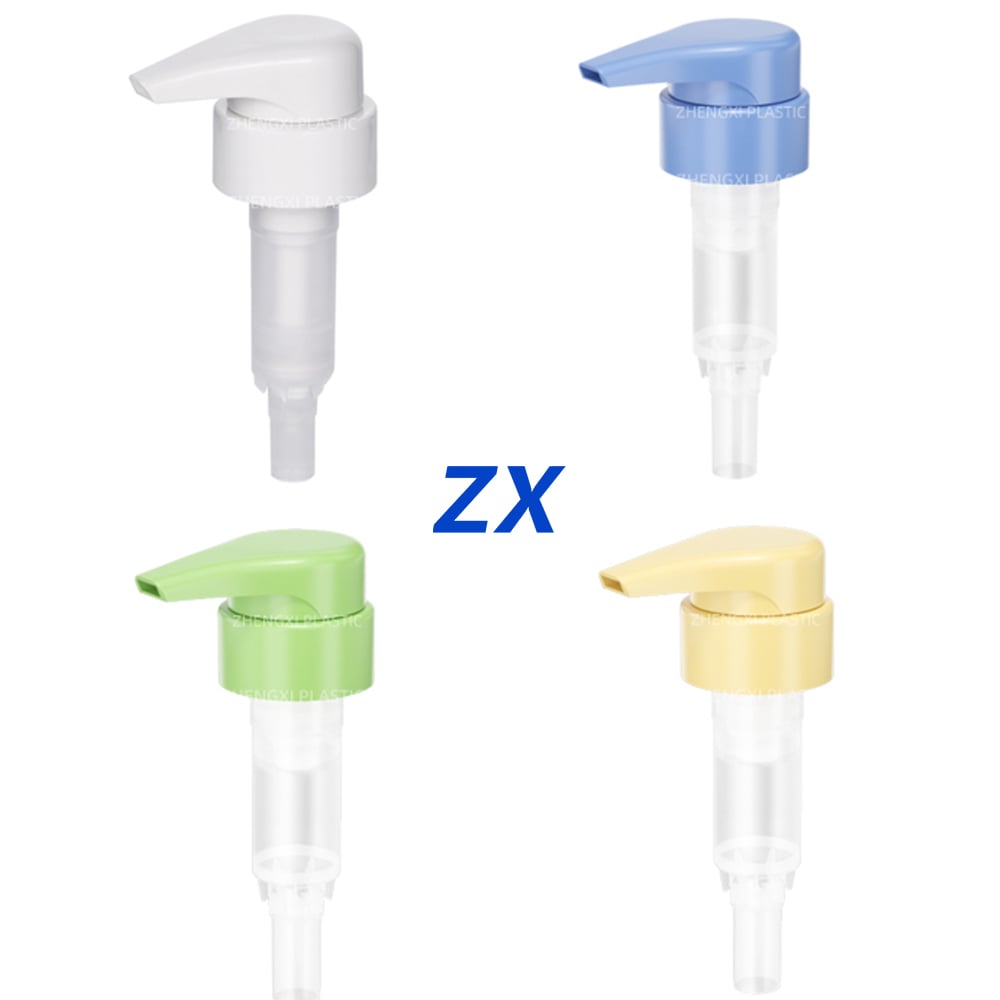
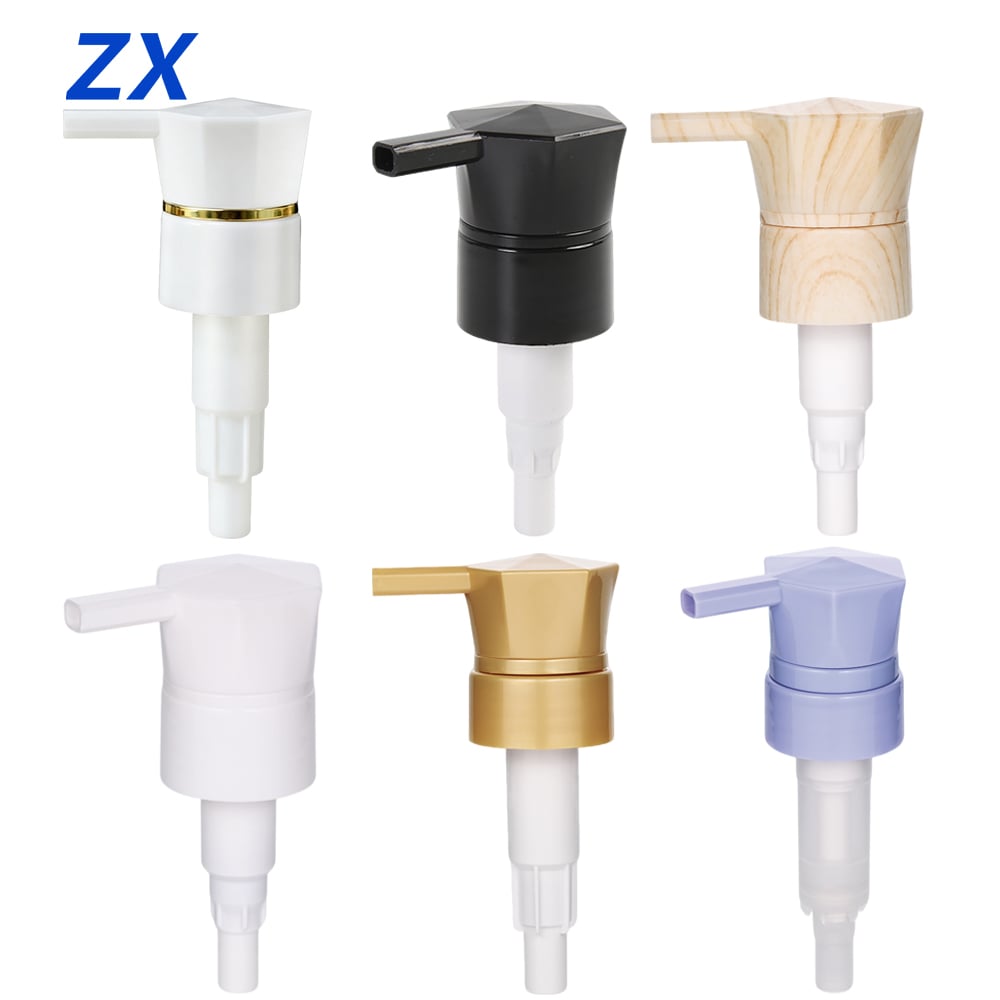
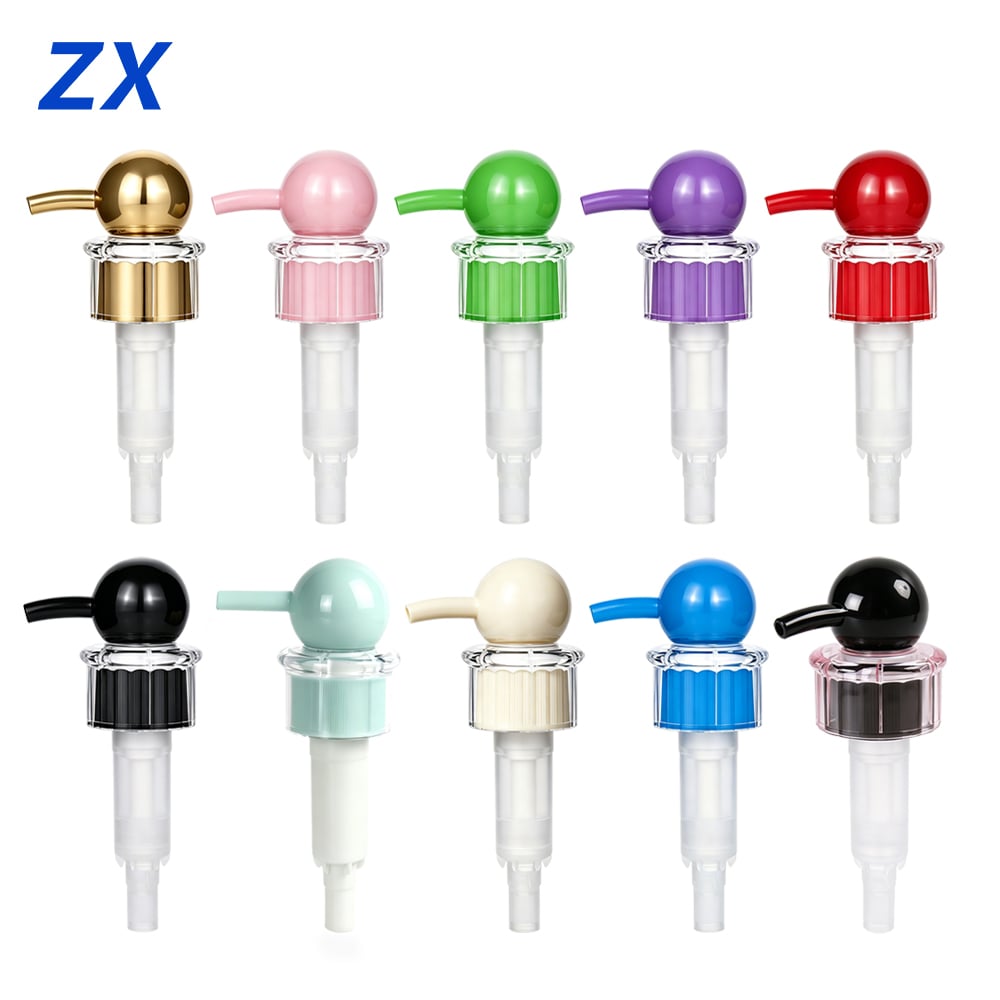
Leading shampoo pump factory operations offer extensive customization capabilities that transform standard dispensers into distinctive brand assets. Color matching services replicate precise Pantone specifications, ensuring pump appearance aligns perfectly with overall packaging aesthetics and brand guidelines. Actuator design modifications create unique tactile experiences, from ergonomic curves that improve grip comfort to decorative elements that communicate premium positioning. A versatile shampoo pump factory maintains tooling capabilities for various closure sizes, accommodating bottle neck finishes from 20mm to 28mm diameter specifications. Output volume customization allows brands to control usage rates, with adjustable stroke volumes that balance consumer convenience against product longevity. Surface finishing options include matte textures that convey natural product positioning or glossy finishes that emphasize luxury attributes. Hot stamping and pad printing technologies available at advanced factories enable logo placement directly on pump actuators, eliminating separate labeling steps and reducing production complexity. These customization services from a shampoo pump factory empower brands to create cohesive packaging systems that strengthen market recognition and justify premium pricing strategies while maintaining the functional reliability consumers expect from quality dispensing mechanisms.
Sustainable Solutions and Environmental Responsibility

Sustainable Solutions and Environmental Responsibility

Progressive shampoo pump factory facilities now prioritize environmental sustainability through material innovation and circular economy principles. Recycled plastic content options reduce virgin resin consumption without compromising structural integrity or chemical resistance, appealing to environmentally conscious brands and consumers. Design-for-disassembly approaches enable end users to separate pump components for proper recycling, with clearly marked material identification codes on each part. Some shampoo pump factory operations have developed fully recyclable mono-material pumps that eliminate mixed-plastic complications in recycling streams. Refillable pump systems represent another sustainable innovation, with durable construction designed for multiple product refills that dramatically reduce packaging waste over the product lifecycle. Lightweight engineering reduces material usage and transportation emissions without sacrificing performance standards. Factory energy efficiency initiatives, including solar installations and waste heat recovery systems, minimize the carbon footprint associated with pump manufacturing. Water-based printing inks and solvent-free adhesives eliminate volatile organic compound emissions during decoration processes. By selecting a sustainability-focused shampoo pump factory, brands demonstrate authentic environmental commitment that resonates with modern consumers while potentially qualifying for green certification programs that enhance market positioning and open access to environmentally focused retail channels.

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000